 admin
As global environmental regulations become increasingly strict and industrial waste grows in complexity, companies across chemical, pharmaceutical, petrochemical, and manufacturing sectors are searching for safer and more efficient treatment methods. Among the available technologies, waste liquid incineration has emerged as one of the most reliable and effective solutions for managing hazardous organic liquids, chemical residues, and toxic by-products.
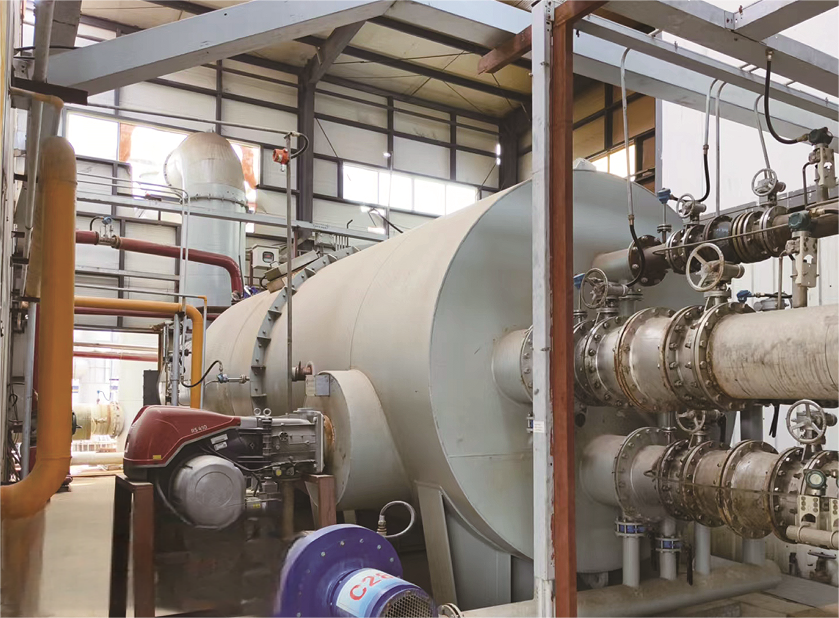
Modern waste liquid incineration systems offer complete destruction of harmful substances, high thermal efficiency, and compliance with demanding environmental emission standards. Companies like Aoli Environmental Protection Technology Co., Ltd., a professional manufacturer of advanced incinerators, are driving this transformation with cutting-edge equipment designed for various types of hazardous wastes—including organic waste gas, waste liquid, medical waste, and dangerous chemical waste.
This article explains why industries around the world are increasingly choosing waste liquid incineration as their preferred hazardous waste treatment method—and how Aoli’s technologies support safe and sustainable operations.
Growing Industrial Demand for Safe Hazardous Waste Disposal
Industrial production generates a wide variety of liquid wastes such as:
-
Toxic organic solvents
-
Contaminated wastewater containing chemical residues
-
Flammable or corrosive liquids
-
Pharmaceutical by-products
-
Petrochemical waste streams
If not properly treated, these substances can contaminate water, soil, and air, posing serious environmental and health risks. With regulatory agencies worldwide enforcing stricter disposal standards, industries need a treatment method that guarantees safe and thorough destruction.
Waste liquid incineration provides exactly that.
Key Reasons Industries Choose Waste Liquid Incineration
1. High Destruction Efficiency (Up to 99.99% DRE)
Incineration operates at extremely high temperatures—often above 1100°C—breaking down hazardous organic molecules completely. This ensures:
-
Destruction of toxic chemicals
-
Minimal harmful residues
-
Prevention of secondary pollution
Aoli’s waste liquid incinerators are engineered to deliver high destruction efficiency through optimized combustion chambers, advanced burners, and precise air supply systems.
2. Suitable for a Wide Variety of Hazardous Liquids
Unlike many treatment methods that work only for specific substances, waste liquid incineration handles diverse waste types, including:
-
High-viscosity organic liquids
-
Flammable solvents
-
Reactive chemicals
-
Medical liquid waste
-
Industrial process liquids
-
Dangerous chemical waste
Aoli Environmental Protection Technology offers different models—such as waste liquid incinerators, process waste incinerators, and rotary kiln incinerators—to meet the needs of different industries.
3. Prevents Environmental Contamination
Other waste disposal methods may leave behind residues, wastewater, or sludge that require further treatment. Incineration reduces liquid waste to:
-
Harmless gases (after purification)
-
Minimal solid ash
With proper gas purification, the risk of soil or water contamination is virtually eliminated.
Aoli’s systems incorporate complete flue gas purification technology, including scrubbers, bag filters, and activated carbon adsorption, to ensure emissions meet or exceed national and international standards.
4. Compatible with Heat Recovery and Energy Reuse
One major advantage of high-temperature incineration is the ability to convert waste heat into usable energy. Many facilities use:
-
Waste heat boilers
-
Hot water generation systems
-
Steam production units
Aoli provides heat energy recovery equipment to help factories reduce energy consumption and improve economic efficiency.
5. Fully Automated and Safe Operation
Modern incinerators are equipped with advanced control technologies such as:
-
PLC/DCS automation
-
Temperature and pressure sensors
-
Flow monitoring
-
Emergency shutdown protection
-
Real-time emission monitoring
Automation reduces human error and ensures stable, safe operation. Aoli’s systems are designed with robust safety features to handle even the most dangerous chemical wastes.
6. Compliance With International Emission Standards
Industries face growing compliance pressure from regulations such as:
-
EU Industrial Emissions Directive (IED)
-
EPA hazardous waste combustion rules
-
National environmental protection standards
Waste liquid incineration is one of the most effective methods to meet these requirements. Aoli’s incinerators—whether waste gas incinerators, pyrolysis furnaces, RTO regenerative thermal oxidizers, or rotary kiln systems—are built to support highly regulated industries.
7. Versatility Across Industries
Waste liquid incineration is widely used in:
-
Chemical factories
-
Pharmaceutical plants
-
Petrochemical refineries
-
Paint, coating, and resin producers
-
Medical and laboratory facilities
-
Hazardous waste treatment centers
Aoli Environmental Protection Technology provides customized solutions based on waste type, production scale, and emission standards.
Aoli Environmental Protection Technology: Leading the Future of Hazardous Waste Treatment
With expertise in environmental engineering and waste treatment equipment, Aoli Environmental Protection Technology Co., Ltd. offers a full range of incineration solutions, including:
-
Medical waste pyrolysis incinerators
-
Process waste incinerators
-
Waste liquid incinerators
-
Waste gas incinerators
-
RTO regenerative thermal oxidizers
-
Hazardous waste rotary kiln incinerators
-
Heat recovery systems
Their strong capability in research, manufacturing, installation, and after-sales service allows industries to adopt safe and efficient waste treatment technologies with confidence.
Final Thoughts
Industries worldwide are turning to waste liquid incineration because it delivers:
-
Unmatched destruction efficiency
-
Safety for workers and the environment
-
Compatibility with a wide range of hazardous liquids
-
Energy recovery value
-
Compliance with strict regulations
With advanced engineering and continuous innovation, companies like Aoli Environmental Protection Technology Co., Ltd. are helping industrial facilities achieve sustainable development while ensuring responsible, safe, and environmentally friendly waste treatment.
www.jsalfsl.com
Jiangsu Aoli Environmental Protection Technology Co., Ltd.